Lined valve low fugitive emission solutions help regulate unintended gas leaks from valves, pumps, and other industrial equipment. These releases can negatively impact environmental safety and regulatory compliance. Therefore, facilities must choose appropriate testing standards to ensure their valve systems remain tight.
This guide compares ISO 15848 and TA-Luft to help determine which fugitive emission requirements best match your operational needs.
ISO 15848 is an international standard that was established in 2006. This was implemented because of an increased demand for sustainable valves. The lack of a harmonized regulation to confirm and classify the environmental impact of leakage to the atmosphere from valves was the main motivator behind it.
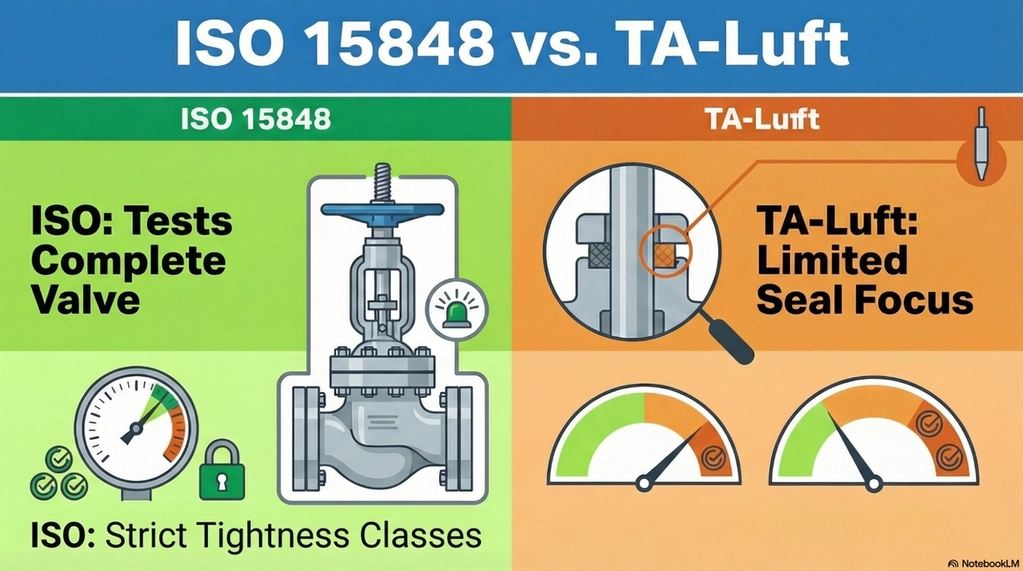
In this framework, the entire industrial valve, including the body seals, will be subjected to type testing. The ISO type test classifies the complete industrial valve into a pressure, temperature, endurance, and tightness class. Its requirements are highly specific and detailed, resulting in a test duration of approximately one to two weeks.
ISO 15848, entitled “Industrial Valves – Measurement, Test, and Qualification Procedures for Fugitive Emissions,” consists of two parts:
Specifying an industrial valve according to ISO 15848 provides the following advantages for purchasers:
The TA-Luft test qualifies only a “high-quality sealing system.” It is a German national directive with the associated test procedure VDI 2440. Established in 1964, this directive was the only widely recognized industry standard for classifying fugitive emission leakage in valves until 2006.
This only defines allowable leakage levels for the stem or gland but does not specify the testing conditions. Rather, it is up to the manufacturer to test the parts under the conditions based on the intended product use. However, this can be considered by the majority as inconsistent, for it will solely rely on each manufacturer’s decision under which conditions leak tests are performed.
The requirements of TA-Luft are very general. Its test duration usually does not take longer than one to two days. There is also no requirement for the number of mechanical cycles or the number of thermal cycles.
Many seal manufacturers promote “TA-Luft packings,” but using this type alone, unfortunately, does not guarantee long-term leak tightness. Overall sealing performance depends on several factors, including stem surface finish and the clearance between the gland and the stem.
| Features | ISO 15848 | TA-Luft |
| Scope | Complete industrial valve | Mainly focuses on sealing system |
| Type | International standard (est. 2006) | German national directive (est. 1964) |
| Testing Method | Type testing with pressure, temperature, and endurance classes | Defines allowable leakage but limited test conditions |
| Tightness Classes | A, B, C (Class A = lowest leakage) | No tightness classification system |
| Mechanical / Thermal Cycles | Required | Not specified |
| Consistency | Standardized and comparable across manufacturers | Mainly focuses on the sealing system |
Selecting between these two standards often relies on the project location and specific client requirements.
ISO 15848 Fugitive Emission Standard remains as widely recognized globally as an efficient and comprehensive testing method. It provides detailed performance data that allows for direct comparison between various valve products. Many international engineering firms now mandate this specific standard for new capital projects.
Meanwhile, TA-Luft is still relevant for facilities operating under German or European environmental permits. Some clients may still prefer it because of long-standing plant specifications and historical documentation. However, it is also important to note that the industry trend is shifting toward adopting the ISO standard for broader compatibility.
Regardless, a lined valve low fugitive emission solution is commonly designed to meet both standards. Precision engineering ensures that the valve packing and body seals achieve the needed tightness levels. Always consult with your valve manufacturer to review their test data and compliance certifications, simplifying your maintenance planning and environmental reports.
Discover our strict quality control and state-of-the-art facilities ensuring the highest standard for every valve.
Explore ProcessManaging fugitive emissions needs a clear understanding of testing standards like ISO 15848 and TA-Luft. The former one provides a comprehensive and internationally accepted method, while the latter one focuses on specific regulatory compliance based on the manufacturer. Both standards reduce leakage while supporting environmental compliance.
Lianke offers lined valve low fugitive emission solutions for demanding environments. As a company with over 20 years of expertise, we continuously maintain strict manufacturing controls and provide our clients with detailed documents and results for both testing standards. Invest in Lianke to ensure the best valve for your specific pressure and temperature conditions.

Valves are everywhere in industrial processes—controlling flow, isolating equipment, and protecting systems from overpressure. Yet for many engineers and technicians, the range of options can feel overwhelming. This guide covers the fundamentals of industrial valves, with a closer look at three widely used types: the lined valve, the pinch valve, and the stainless steel ball […]

Valve installation looks simple on paper—until you’re on-site, the flanges don’t line up, and the process fluid is waiting. In reality, poor installation is one of the leading causes of premature valve failure, leakage, and costly downtime. Whether you’re working with a lined valve, a strainer, or a pinch valve, the same fundamental rules apply. […]

Lianke Valve Co., Ltd. has just wrapped up a busy and rewarding season of site visits. Over the past two weeks, we have hosted several groups of clients from home and abroad. They came with different goals, yet all turned their attention to Lianke’s manufacturing strength and technical expertise. Juhua Group, Quzhou In early March, […]

Recently, the production workshop at Lianke Valve has been bustling with activity, where production, inspection, packaging and other processes operate in efficient coordination. After rigorous multi-stage quality checks, a batch of high-quality pinch valve products has been packed and shipped, setting off for Russia. Export Product Case The pinch valves in this bulk shipment are […]