Some of the top valve manufacturers Russia brought to NEFTEGAZ Moscow 2024 include names like Fluid-Line, NT Valve, and Dombor Valve, along with others.
Each of these companies plays a part in supplying the Russian oil gas valves market, from isolation and control valves to fully automated flow systems.
Below, we take a closer look at the key exhibitors and their role in Russia’s growing industrial supply base.
Here’s a quick look at the companies that made a statement on the show floor:
| Company | Type of Valves | Main Focus |
| Fluid-Line | Control, Safety | Pipeline control, local supply |
| NT Valve | Isolation, Control | Harsh media, energy sector |
| Dombor Valve | Gate, Globe, Ball | Heavy-duty oilfield service |
| WZ-VALVE JSC | Isolating, Shutoff | Crude oil and chemical service |
| Samson Controls | Automated Control | Process automation |
| TREM Engineering | Engineered Valves | Custom seals, high pressure |
| ABS ZEiM Automation JSC | Automated, Control | Integrated valve systems |
Fluid-Line makes safety and control valves built for Russian pipeline systems. At NEFTEGAZ 2024, the company showcased locally produced valves designed for high-pressure flow and rugged outdoor conditions. This focus on domestic manufacturing aligns with national goals to reduce reliance on imported infrastructure parts.


NT Valve manufactures isolation and control valves for aggressive fluids and extreme heat. These products are commonly used in refinery loops, chemical plants, and power installations. During the event, the company introduced updated models aimed at helping operators reduce unplanned maintenance and downtime.

Dombor returned to NEFTEGAZ with its range of heavy-duty gate, globe, and ball valves. These valves are built for midstream oil transport and large-volume pipelines. Visitors to the booth saw material and design features tailored for pressure-intensive service over long distances.

WZ-VALVE JSC specializes in isolating and shutoff valves used in crude oil, gas, and chemical systems. The product line supports both aboveground installations and buried pipeline networks. The company’s focus on long-life equipment matches the needs of tank farms and export terminals.

Samson is widely known for smart control valves used in process automation. At NEFTEGAZ, the team showcased systems designed for gas processing, compressor stations, and complex refinery networks. Demos included integrated diagnostics and position feedback built directly into the valve assemblies.

TREM Engineering develops high-pressure valves and sealing solutions for demanding field conditions. The company works closely with Russian oilfield operators to match valve specs with well-site needs. Its 2024 display focused on reliability in corrosive and high-temperature environments.

ABS ZEiM builds automated valve systems with real-time monitoring capabilities. These setups help plants control flow and check valve status from a central dashboard. At the exhibition, the company highlighted how its integrated systems simplify process control across oil, gas, and chemical facilities.
Each of these companies brought forward solutions tailored to Russia’s oil and gas infrastructure needs. From automation to pressure handling, the focus was on performance that fits local conditions and supply expectations. If you’re sourcing valves within the region, these are proven suppliers already active in the field.
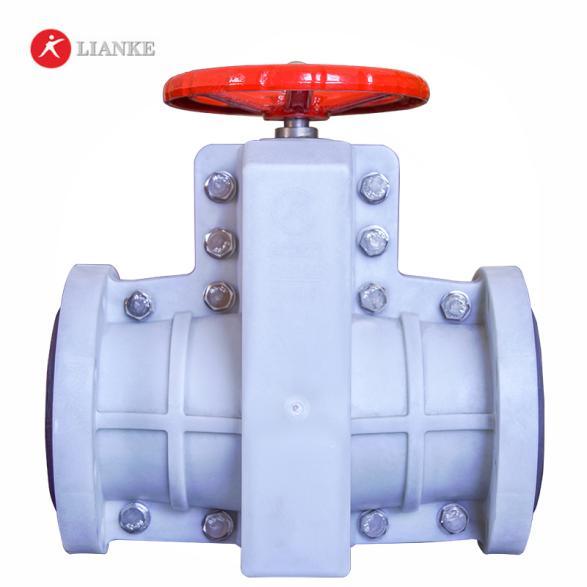
PP pinch valve, as the name suggests, is a pinch valve of PP shell material. The main advantage of this valve is that the valve body is made of pp plastic, so the valve body is lighter and can be installed on the suspended pipe. PP material has the characteristics of acid and alkali resistance […]

Basket strainers are essential pipeline pre-filtration equipment widely used in chemical processing, water treatment, petroleum, food & beverage, pharmaceutical and general manufacturing. Industrial fluid pipelines are critical to stable production, yet process water, oil and chemical media often carry sediment, rust, solid particles and material agglomerates. These tiny contaminants cause pump abrasion, valve blockage, heat exchanger […]
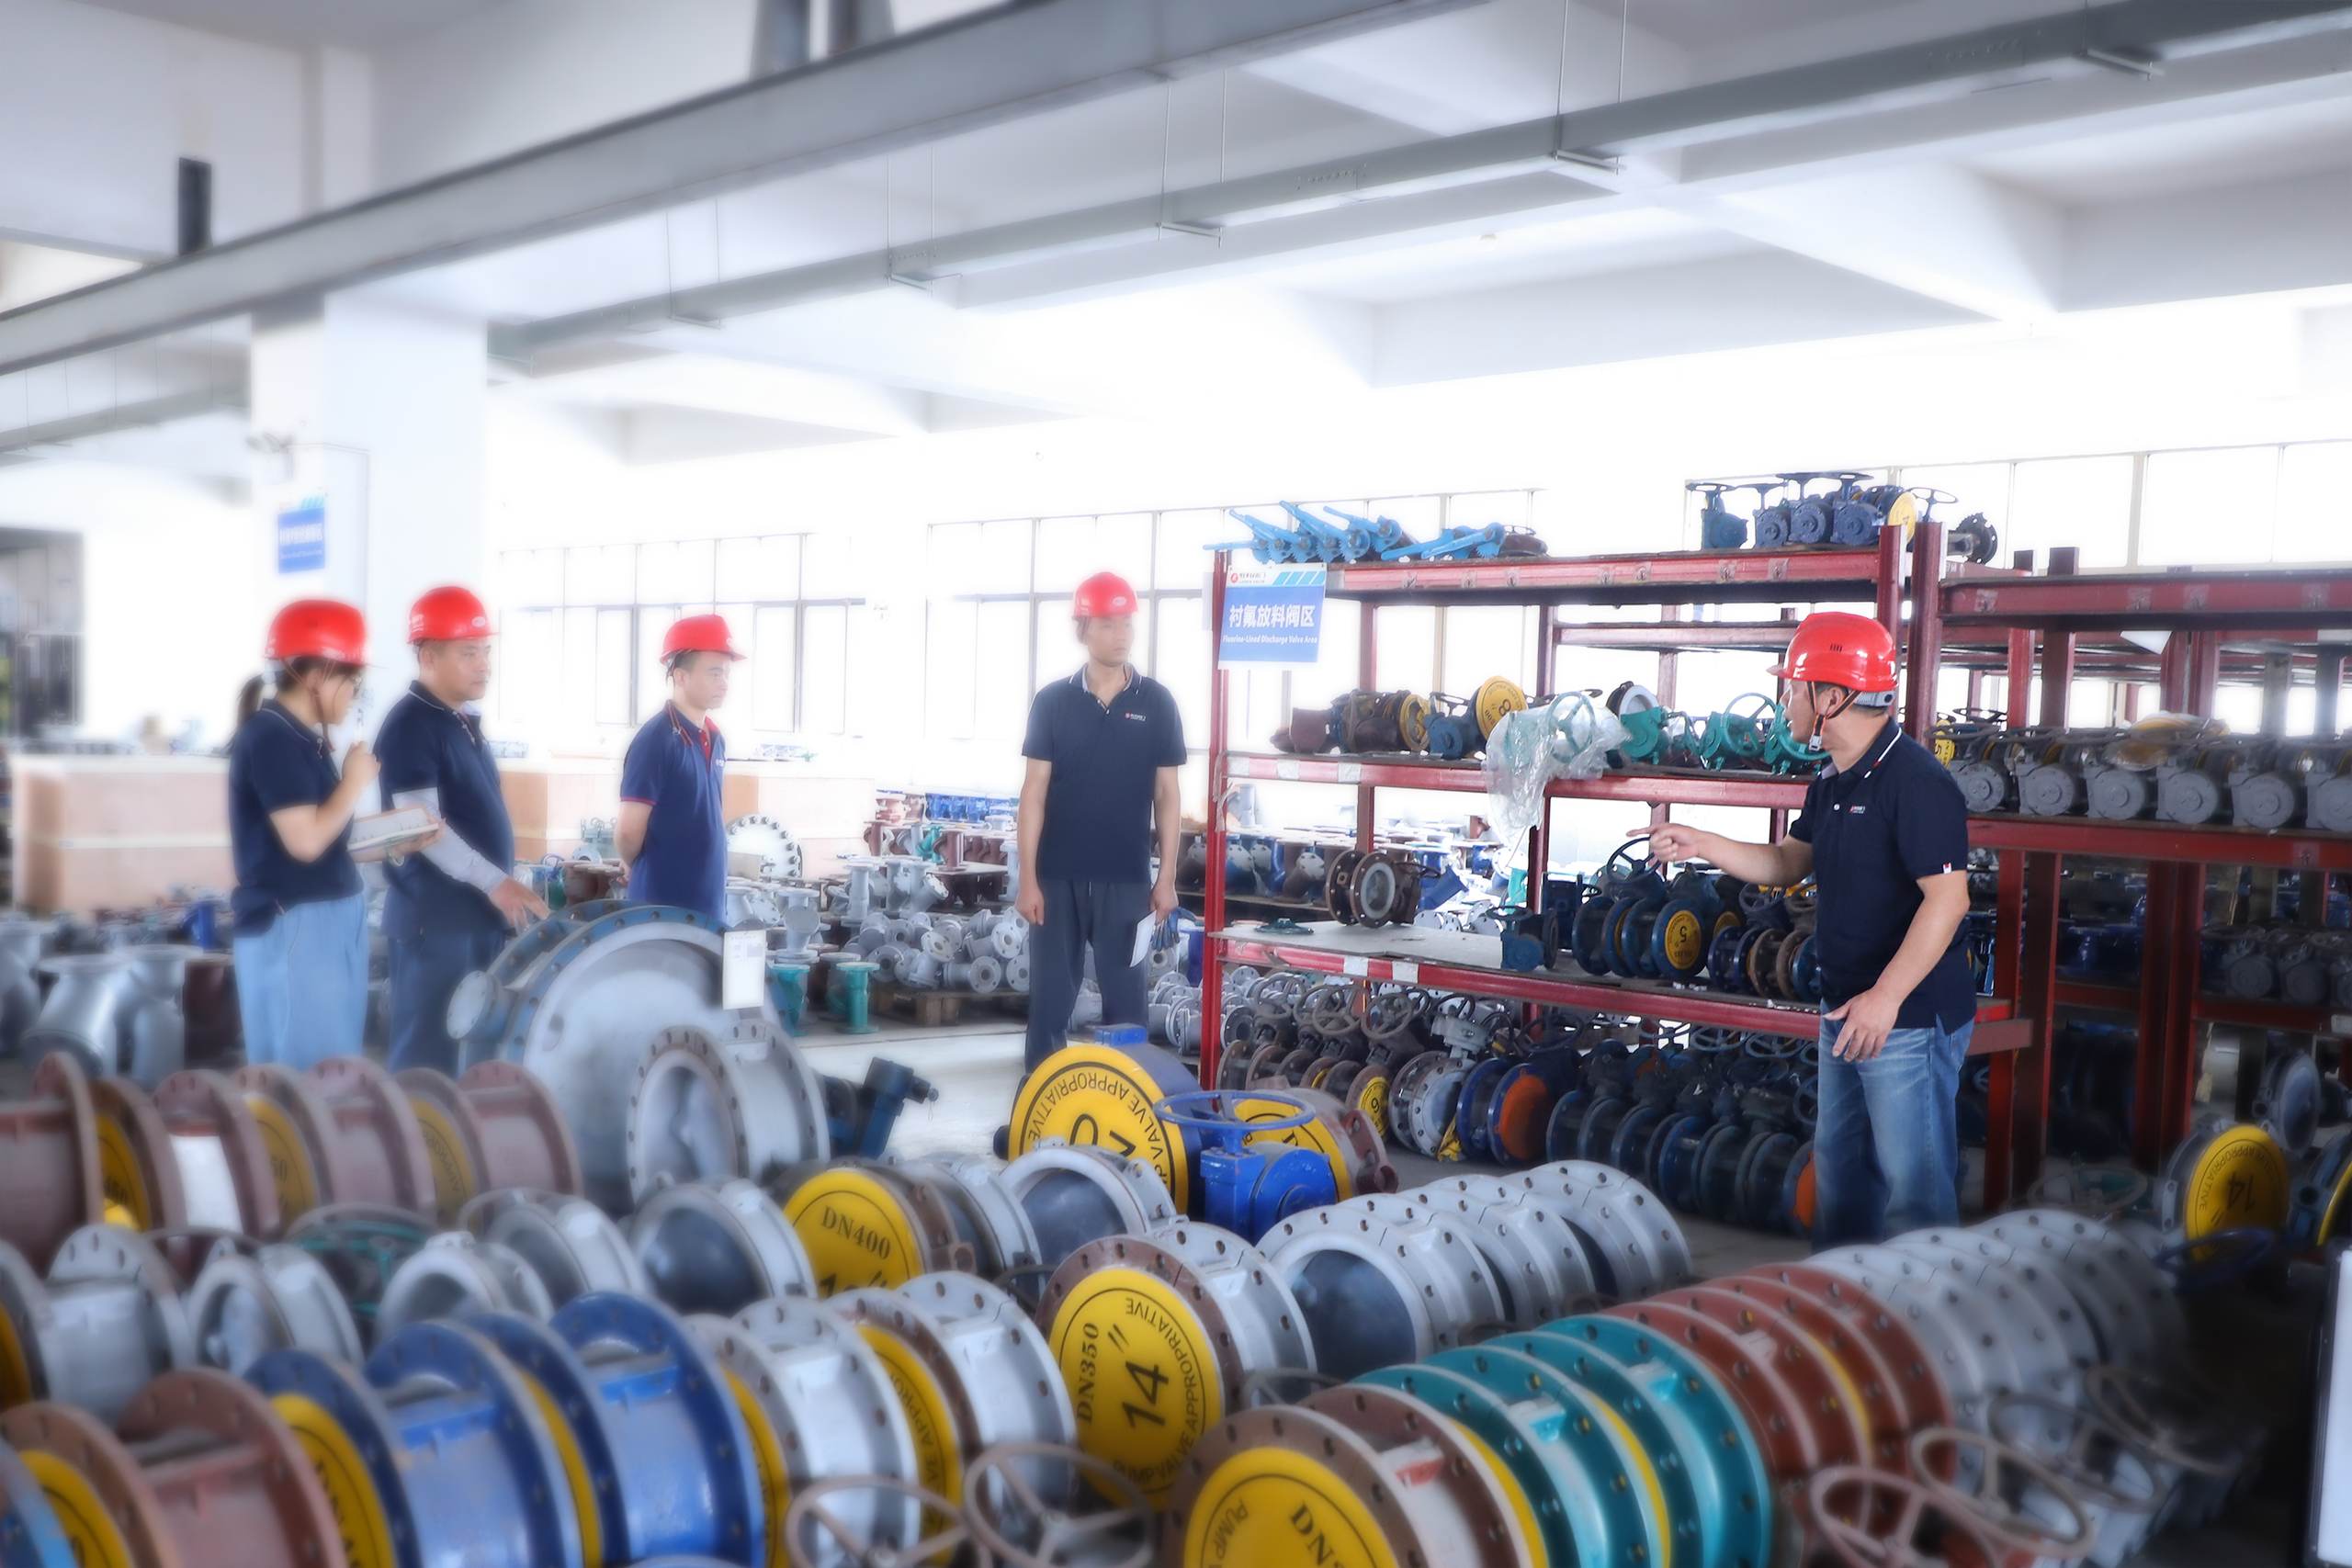
In 2026, Lianke Valve marks the 25th national Work Safety Month. Centered on the theme “Guard the bottom line by addressing minor risks; build safety through rigorous inspection and rectification”, Lianke Valve has fully launched a special work safety campaign. By implementing a full range of activities including thematic briefings, emergency drills and hazard inspections, […]
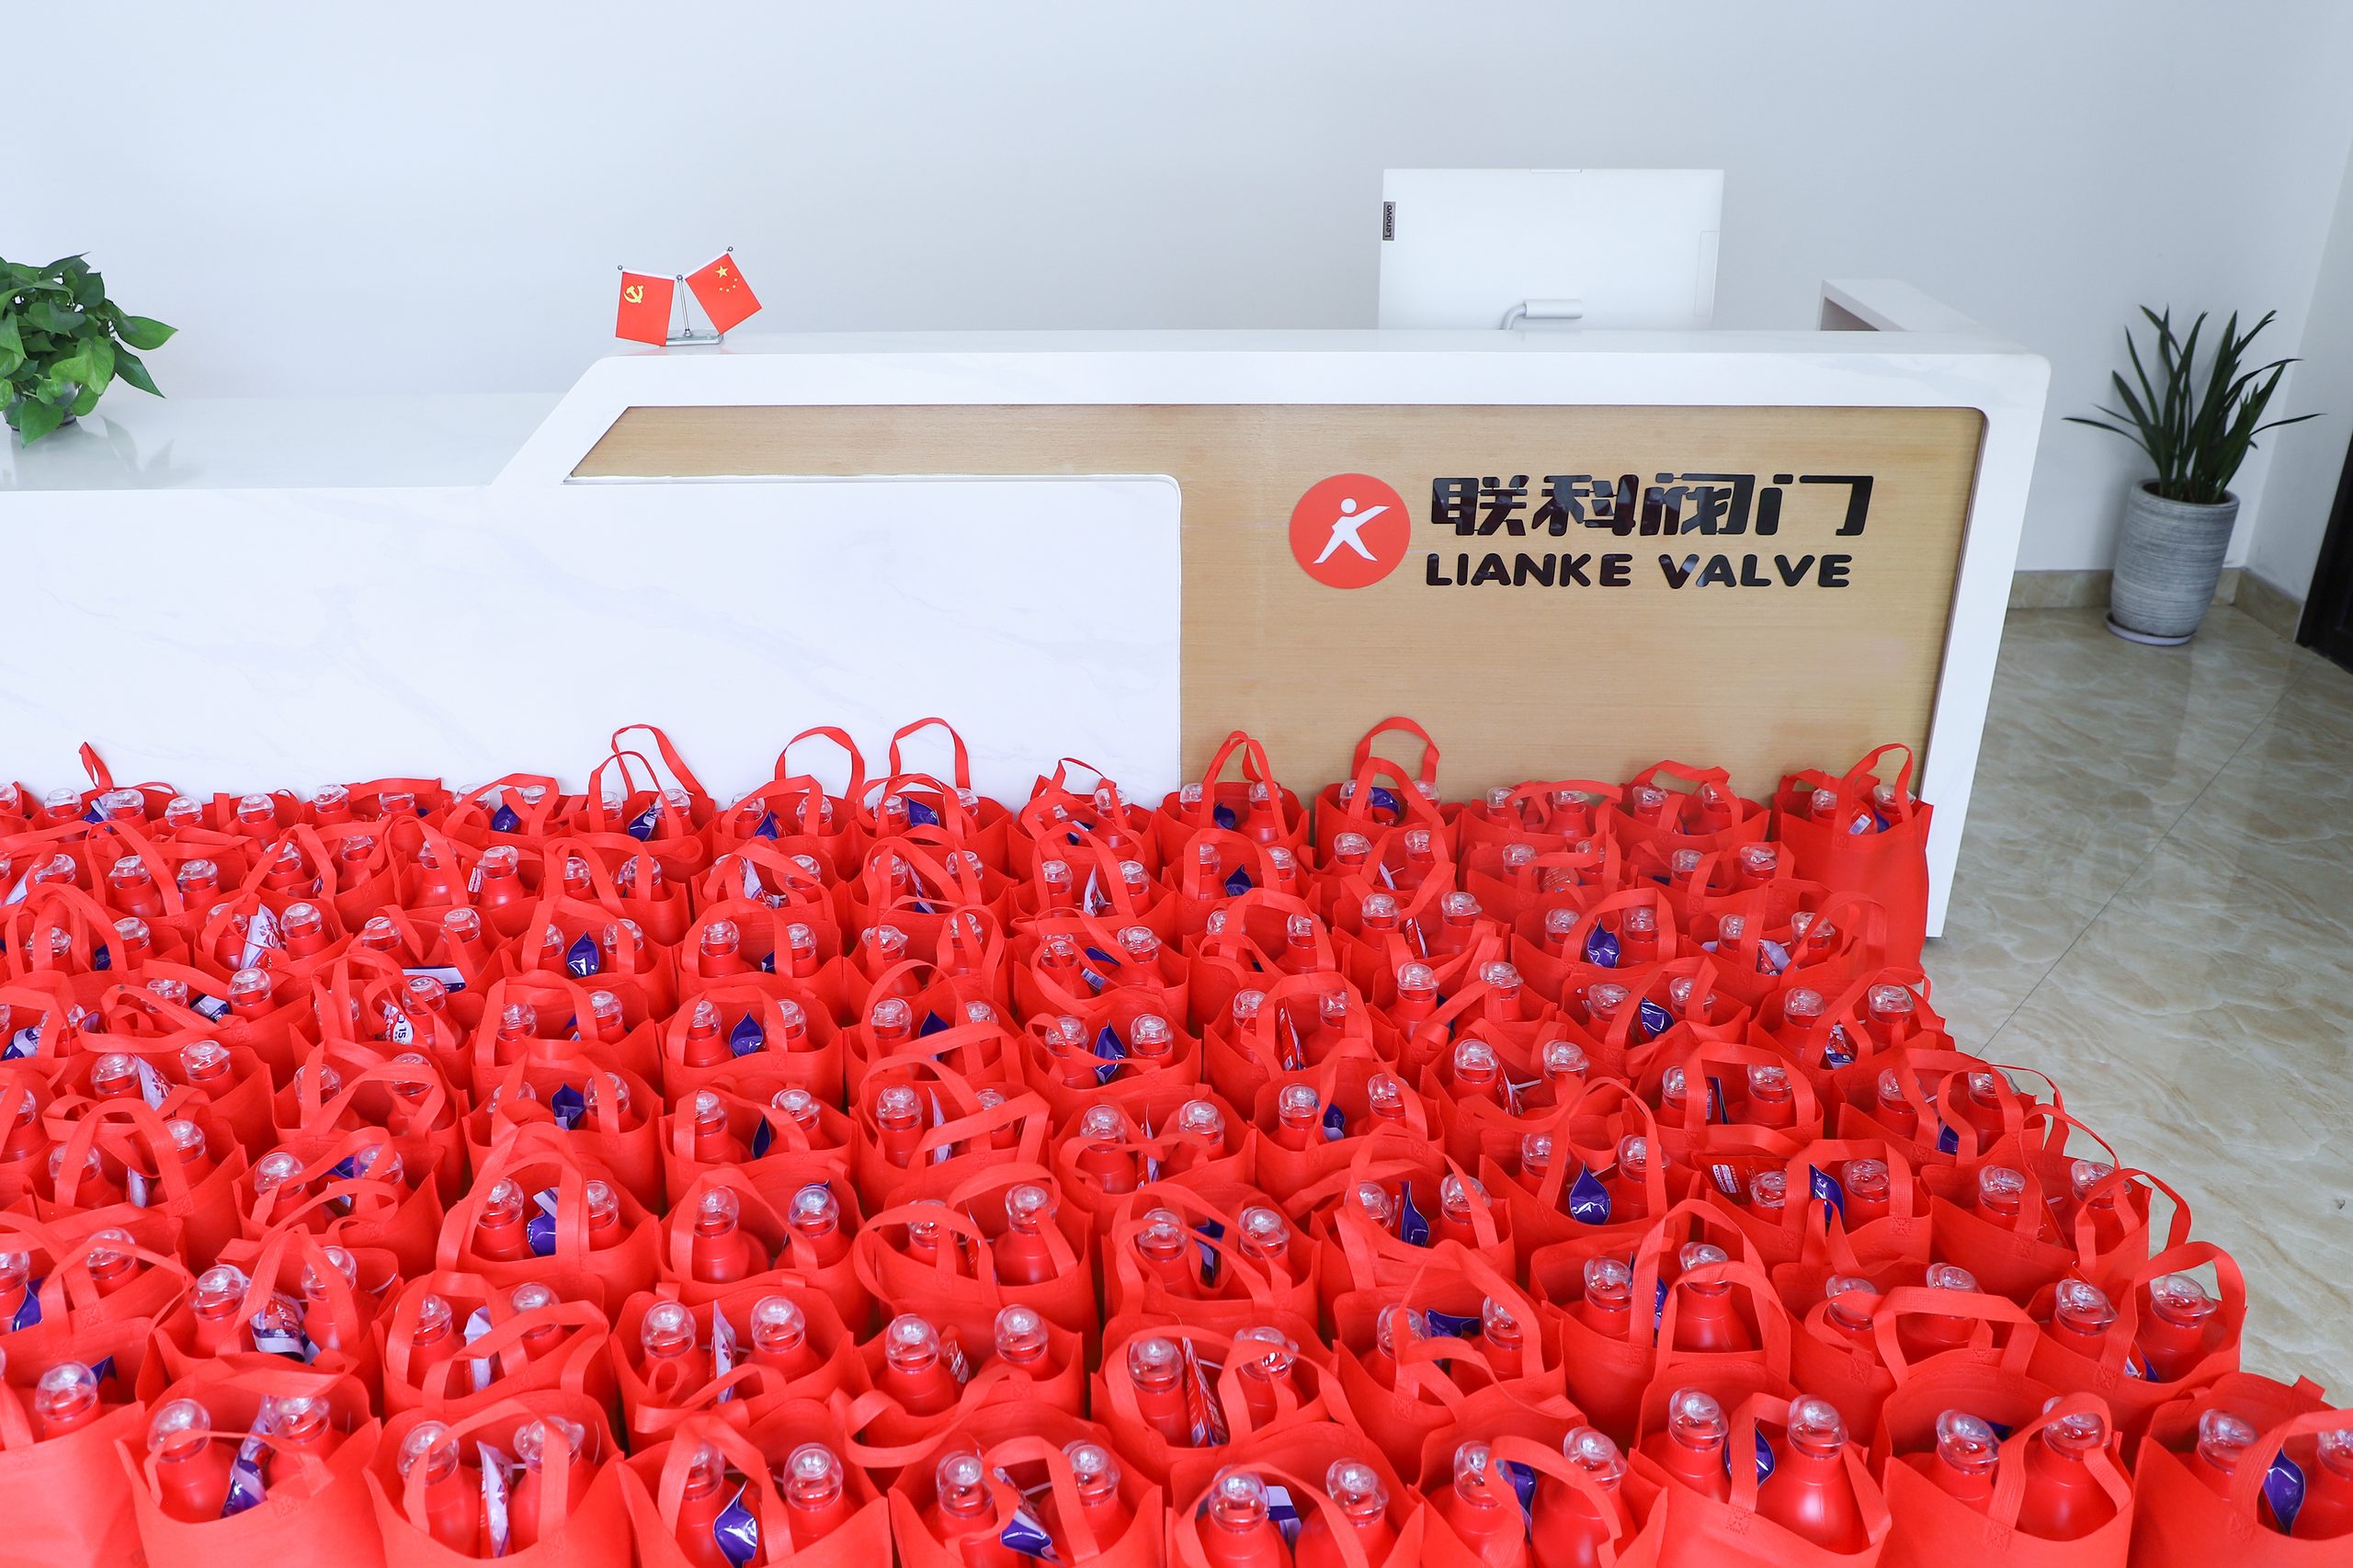
As intense summer heatwaves continue, persistently high temperatures have brought severe challenges to frontline workshop operations. To effectively conduct heatstroke prevention work and protect the physical and mental health of all employees, Lianke has launched the annual Summer Cool Relief employee care campaign. Honoring Dedication with Sincere Care The company has distributed daily-use laundry detergent […]


